Recyclable Packaging Tapes: Technical Guide for Buyers
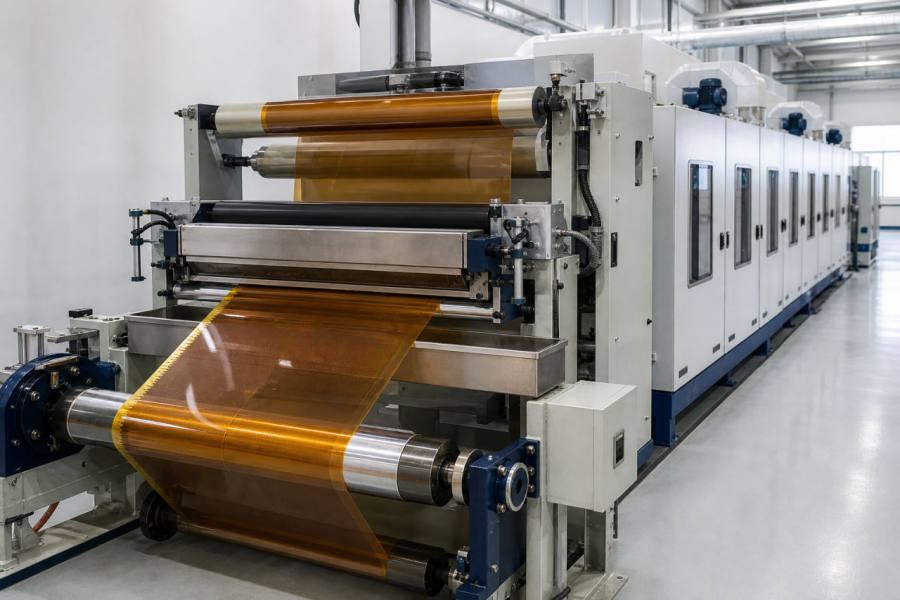
European packaging regulations are moving rapidly from high-level targets into concrete technical specifications. On 8 September 2026, Afera (the European Adhesive Tape Association) announced the launch of a dedicated Task Force on Packaging Tapes under the emerging CEN Design for Recycling (DfR) framework to support the European Packaging and Packaging Waste Regulation (PPWR). The initiative brings technical experts together to establish how pressure-sensitive adhesive (PSA) tapes are tested, classified, and handled during paper and corrugated recycling streams. For industrial buyers, exporters, and logistics managers sourcing packaging tapes from Chinese manufacturers, this regulatory shift creates a practical challenge: how to maintain high-strength box closure while ensuring the tape does not compromise the recyclability score of secondary packaging.
1. Why Tape Design Governs Cardboard Box Recyclability
When a corrugated shipping carton reaches a paper recycling plant, it is mixed with water and mechanically agitated in a hydrapulper to separate wood fibers from non-paper contaminants. In traditional operations, conventional plastic packaging tapes and adhesives can create persistent problems during this repulping cycle:
- Stickies Formation: Pressure-sensitive adhesives (PSAs) that fragment into tiny particles (micro-stickies) during pulping pass through coarse screening screens. Under downstream heat and pressure on paper-making rollers, these adhesive particles re-agglomerate, sticking to drying cylinders and causing costly web breaks or paper blemishes.
- Screening Efficiency: If an adhesive remains intact on its carrier film during low-temperature pulping, it can be screened out mechanically as a large particle. However, if the adhesive softens and disperses into the pulp slurry, chemical treatment or expensive flotation processes are required to remove it.
- Fiber Yield Loss: Tapes that require aggressive mechanical shearing to remove from cardboard often tear usable surface fibers, reducing the overall yield of recycled pulp.
Under Europe's evolving DfR criteria, packaging components—including closing tapes—must be compatible with standard recycling mills without disrupting paper quality or generating problematic stickies.
2. Carrier Film vs Adhesive Chemistry: The Recyclability Breakdown
A packaging tape's recyclability profile is determined by two distinct layers: the backing material (carrier) and the adhesive formulation. Understanding how each behaves in a paper recycling mill is essential for technical procurement:
Backing Substrates
1. BOPP (Biaxially Oriented Polypropylene): The standard carrier for high-volume carton sealing. In standard paper recycling, BOPP film does not dissolve in water. It floats to the top during flotation screening and is mechanically separated. While the plastic film itself is not repulped into paper, its high wet tensile strength allows it to be removed cleanly without shredding into micro-fibers, provided the adhesive does not disperse. 2. Kraft Paper Backing: Paper-backed tapes offer aesthetic consistency with corrugated cartons. However, non-reinforced paper tapes may have lower tensile strength than film tapes, requiring heavier basis weights for heavy-duty shipping. 3. Fiberglass-Reinforced Filament Tapes: Filament tapes embed continuous glass yarn filaments into polyester or polypropylene films. They provide exceptional cross-direction tensile strength for pallet bundling and heavy carton closure. In recycling streams, the continuous filaments remain intact and are easily captured by coarse screeners without entering the fine pulp fraction.
Adhesive Formulations
- Water-Based Acrylic Adhesives: Formulated with synthetic polymers dispersed in water. When engineered for recycling compatibility, high-cohesion acrylics resist breaking down into micro-stickies during pulping and maintain clean fiber release.
- Synthetic Rubber / Hot-Melt Adhesives: Offer aggressive initial tack and rapid bonding to recycled corrugated liners. They perform reliably in automated high-speed case sealing, but require specific cohesive strength to avoid gummy contamination in warm pulping baths.
3. Heavy-Duty Sealing vs Recyclability: Striking the Operational Balance
For manufacturers of industrial equipment, automotive parts, and consumer appliances, carton sealing performance cannot be compromised for sustainability claims. An under-specified tape that fails during maritime shipping causes carton burst, moisture ingress, and product damage—creating a much larger environmental and economic cost than the packaging material itself.
To achieve both carton integrity and recycling compliance, industrial buyers should evaluate three operational parameters:
1. Holding Power (Shear Resistance): A packaging tape must resist continuous shear stress along carton flaps during container vibration and stacking. High shear resistance ensures the box remains closed under transit stress without requiring excessive tape layers. 2. Substrate Tack on Recycled Liners: Recycled corrugated board contains shorter paper fibers and often has a rougher, more porous surface than virgin kraft liner. The tape adhesive must achieve sufficient wet-out and mechanical interlocking on high-recycled-content board without requiring excessive application pressure. 3. Application Temperature Window: If cartons are sealed in unheated winter warehouses or packed hot from assembly lines, the adhesive must maintain viscoelastic grip across the entire temperature spectrum without hardening or bleeding.
4. Four Key Questions for Your Packaging Tape Supplier
When requesting custom tape quotations or factory audits for export packaging lines, provide clear technical parameters rather than generic requests for 'eco-friendly tape':
1. What is the carrier substrate and total thickness? Request individual specifications for film thickness (e.g., 25μm, 28μm, 35μm) and adhesive coating weight (g/m²) to verify structural integrity. 2. What adhesive technology is used? Clarify whether the formulation is water-based acrylic, hot-melt synthetic rubber, or solvent-based, and request technical data sheets confirming cohesive strength. 3. Is technical documentation available for destination compliance? Ensure the manufacturer can supply material safety declarations, RoHS/REACH compliance documentation, and SVHC screening certificates for European or North American customs clearance. 4. Can custom roll dimensions and winding be provided for automated case sealers? High-volume export lines require consistent machine-roll lengths (e.g., 990m or 1500m rolls) with controlled unwinding noise and uniform edge slitting to prevent line stoppages.
5. Practical Checklist for Export Packaging Compliance
To prepare packaging operations for 2026/2027 international compliance updates:
- Audit current carton closure methods across all product lines (manual hand dispensers vs automated case sealers).
- Standardize on tape widths that provide adequate flap coverage (48mm or 72mm) in a single pass, eliminating redundant cross-taping.
- For heavy or hazardous cargo (>25 kg), evaluate fiberglass filament reinforced tapes to replace plastic strapping or multiple overlapping film layers.
- Request batch-traceable certificates of analysis (COA) from your tape converter to ensure adhesive formulation consistency across export shipments.
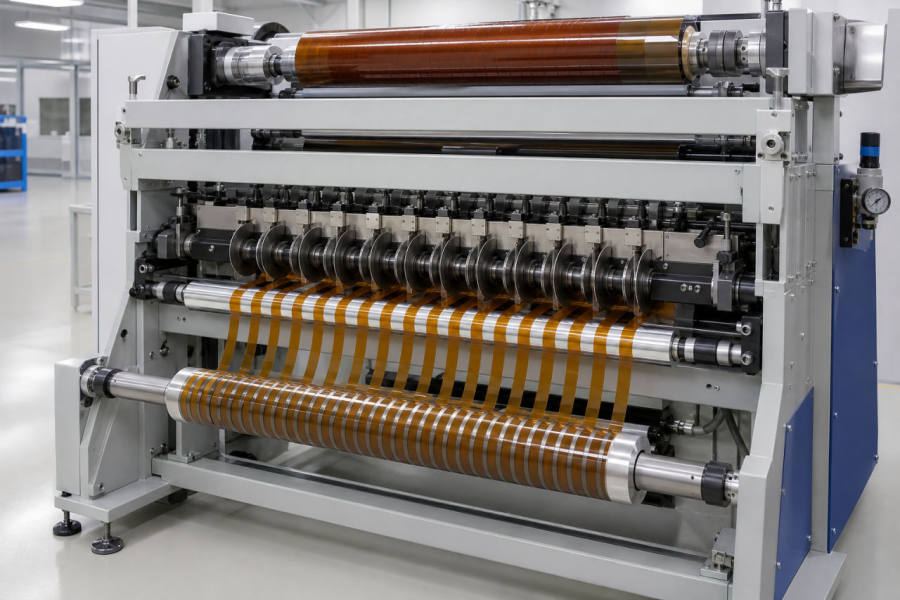
At Many Tape, we manufacture custom packaging and industrial adhesive tapes engineered for demanding export applications. With in-house precision coating, slitting, and die-cutting capabilities, we supply high-performance carton sealing, filament reinforcement, and custom-printed tapes directly from our Dongguan factory. Contact our technical team today to discuss specifications, custom widths, and sample evaluations for your export packaging lines.